


What You’ll Learn
- The six risk control methods of Table F.3, ranked from most effective to least effective
- What each level does, with the annex’s own examples — including swapping 120 V control circuitry for 24 V
- Why the hierarchy must be worked in descending order, not picked from like a menu
- How the apply–evaluate–reapply loop runs until the remaining risk is acceptable
- Why elimination and substitution are easiest and cheapest at the design stage, and why PPE is deliberately last
A Ladder, Not a Menu
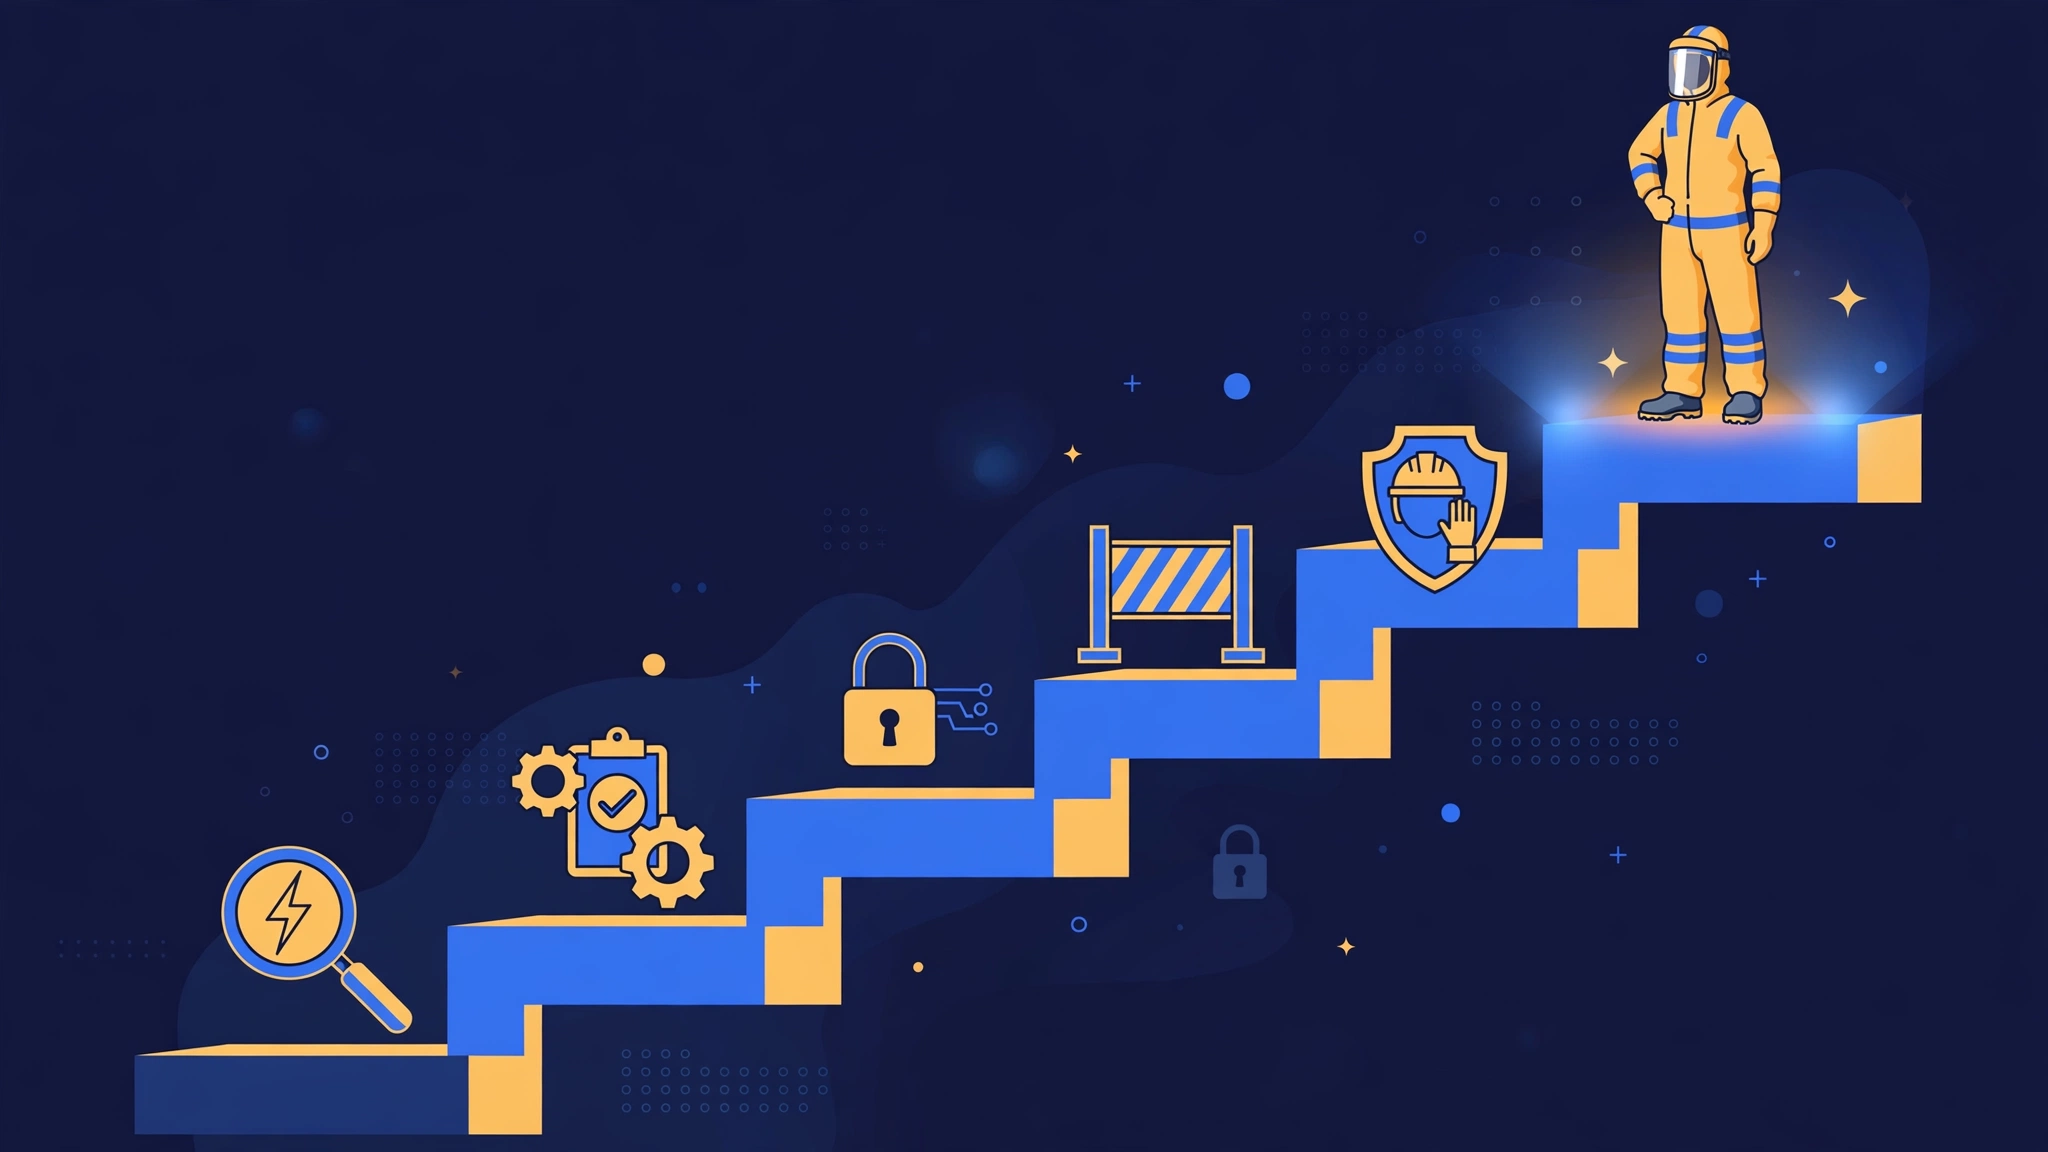
When a risk assessment shows that a hazard can hurt someone, the next question is what to do about it — and Informative Annex F.3 answers with an ordered list. The hierarchy of risk control ranks six methods from most effective to least effective, and the ranking is the point. Each method lower on the list is considered less effective than the one above it, so the assessor starts at the top and works down, asking at each level whether that control can eliminate the hazard or reduce the risk. Only after the higher levels have been applied — or honestly found not to apply — does the assessor reach for the levels below. Risk can be driven down significantly this way, even though the annex is candid that risk can never be erased entirely. Whenever the remaining risk is still unacceptable, more controls must be added until it is brought to an acceptable level for the task at hand.
Table F.3 lays the ladder out:
| Rank | Risk control method | Example from Table F.3 |
|---|---|---|
| (1) | Elimination | Conductors and circuit parts placed in an electrically safe work condition |
| (2) | Substitution | Lowering energy by replacing 120 V control circuitry with 24 Vac or Vdc control circuitry |
| (3) | Engineering controls | Guarding energized conductors and circuit parts to reduce the chance of contact or arcing faults |
| (4) | Awareness | Signs warning of the potential presence of hazards |
| (5) | Administrative controls | Procedures and job planning tools |
| (6) | PPE | Electric shock and arc flash protective equipment |
Elimination: The Hazard No Longer Exists
Elimination sits at the top because it is the only level that removes the hazard itself rather than managing people’s exposure to it. In the electrical context, the annex’s example is placing conductors and circuit parts in an electrically safe work condition — de-energized, tested, and grounded as required — so that the electrical hazard is simply not there while the work happens. Done at the design stage, elimination can go further: equipment can be laid out so that a task never requires exposure in the first place.
The annex also draws an honest distinction. For equipment that is already installed, true elimination is often not available — the gear exists, it must run, and someone must maintain it. Putting equipment into an electrically safe work condition achieves the same end state for a particular job, but it is reached by applying other controls, and every step of that process carries its own chance of human error. That is why the annex insists the first attempt should always be genuine elimination, or substitution to shrink the hazard, rather than settling early for controls that depend on people doing everything right every time.
Substitution: Same Job, Less Energy
Substitution replaces something hazardous with something less hazardous that does the same job. Table F.3’s example is a control-voltage trade: replacing 120 V control circuitry with 24 Vac or Vdc control circuitry. The machine still gets its control signals, but the voltage a technician can contact during troubleshooting drops to a level with far less shock potential behind it. Nothing about the task changes except the size of the hazard attached to it.
Substitution is a design-stage tool above all. Swapping a control transformer and a set of relays on a drawing is trivial; retrofitting a built and wired panel is a project. The annex makes the broader point that during system design and equipment selection it is far easier to reach for the top of the hierarchy — elimination and substitution — to limit the risk that will attach to whatever energized work is later justified.
Engineering Controls: Built Into the Equipment
Engineering controls are physical features designed into the equipment that reduce the likelihood of contact or of a fault occurring. Table F.3’s example is guarding energized conductors and circuit parts so that fingers, tools, and dropped hardware cannot easily reach them or bridge them into an arcing fault. Covers, barriers, insulated or shrouded parts, and enclosures all work this way: they do not depend on the worker remembering anything, which is exactly why they rank above every control that does.
Because they are built in, engineering controls share substitution’s timing lesson — they are cheapest and most effective when specified before purchase. A guard that is part of the original equipment protects every worker for the life of the gear; a guard improvised afterward protects only as well as the improvisation.
Awareness: Making the Hazard Visible
Awareness controls tell people a hazard is present so they can behave accordingly. Table F.3’s example is signs alerting workers to the potential presence of hazards — arc flash and shock warning labels, boundary markings, and equipment identification all serve this purpose. An awareness control changes nothing about the hazard itself; it changes what the person approaching the equipment knows, and therefore what that person does next.
That dependence on human response is why awareness ranks fourth rather than higher. A sign only works on someone who sees it, understands it, and acts on it. It is a necessary layer — the annex’s own risk-evaluation discussion pairs barriers and awareness devices together with other controls — but it is never a sufficient one on its own.
Administrative Controls: Procedures and Planning
Administrative controls govern how the work itself is organized and performed: procedures, job planning tools, permits, briefings, training, and qualification requirements. Table F.3 names procedures and job planning tools as the representative examples. These controls shape behavior at scale — they make sure the right steps happen in the right order, by people prepared to do them — and they are the layer most employers reach for first because they can be created quickly and cheaply.
The hierarchy exists partly to correct that instinct. A procedure is only as strong as its execution on a tired Friday afternoon, under schedule pressure, by someone having a bad day. Administrative controls are essential, and the annex’s evaluation guidance expects them in the mix, but they sit second from the bottom because they rely entirely on people following them.
PPE: The Last Resort, On Purpose
PPE — arc-rated clothing, voltage-rated gloves, face and eye protection, and the rest of the shock and arc flash ensemble — is the sixth and final level. The annex states the reason plainly in substance: PPE is the least effective control and should be selected only after all the other risk controls have been exhausted. It is not the first control, and it must never be the only one.
The logic is unforgiving. Every level above PPE reduces either the hazard or the likelihood of the harmful event. PPE does neither — the arc flash still happens, at full energy, and the equipment merely blunts the injury to the person standing in front of it. When it is under-rated, damaged, or worn incorrectly, there is nothing behind it. PPE absolutely has its place: it is the final layer that protects a worker when residual risk remains after the higher controls have done their work. But starting the assessment at PPE — “just wear the suit” — inverts the hierarchy and leaves the strongest tools unused.
Worked in Descending Order, Then Worked Again
Applying the hierarchy is not a single pass. The annex describes an iterative process: identify the hazard, try the highest control that can apply, evaluate the risk that remains, and then apply the hierarchy again to what is left, repeating until the risk of injury is reduced to an acceptable level. The result of each risk assessment is checked to see whether the hierarchy can be pushed further to lower the risk or shrink the hazard itself.
In practice, most real tasks end with several levels working together — the annex’s evaluation discussion notes that barriers, awareness devices, safe operating instructions, qualification and training, and PPE are often combined, and that all six levels may be needed in some form before the remaining risk is tolerable. The descending order governs the sequence of consideration, not a demand that only one level be used. What it forbids is skipping: deciding on PPE before asking whether the hazard could be eliminated, substituted, or engineered down first.
Why the Design Stage Is Where the Top Is Cheapest
The annex returns to timing repeatedly, and the pattern is economic as much as technical. During electrical system design and equipment selection, elimination and substitution are decisions made on paper — a different control voltage, a different layout, equipment chosen with maintenance exposure in mind. Once the equipment is installed, those same controls become outages, purchase orders, and retrofit labor, if they remain possible at all. A design decision, good or bad, also lasts: the annex’s introduction stresses that how equipment is designed and installed affects the safety of everyone who operates or maintains it for the whole life of the equipment.
That is why the hierarchy’s top two levels belong primarily to designers, specifiers, and purchasers, while its lower levels dominate day-to-day field work. A field crew cannot retroactively substitute a 24 V control circuit during a repair job; it can de-energize, follow the procedure, and wear the PPE. The hierarchy therefore assigns responsibility as well as method — the people who choose the equipment carry the strongest controls, and the assessment should reach them while their choices are still cheap.
Worked Scenario
A plant is replacing the control system on a packaging line, and the risk assessment for future troubleshooting work identifies routine contact exposure to the 120 V control wiring inside the panel. The team works the hierarchy from the top. Elimination: the panel cannot be eliminated — the controls must exist — and while troubleshooting sometimes requires power for diagnostics, most checks can be done de-energized, so the procedure will default to an electrically safe work condition. Substitution: the designers specify 24 Vdc control circuitry in place of the 120 V design, cutting the shock hazard at the source for every future interaction — a line-item change on the purchase order. Engineering controls: the remaining higher-voltage sections get finger-safe, guarded terminals and a dead-front layout. Awareness: the panel gets updated shock and arc flash labels reflecting the new design. Administrative controls: the troubleshooting procedure and job plan are revised for the new equipment. PPE: with the control hazard substituted down, the residual assessment supports a lighter PPE ensemble for the control work than the old panel demanded. Six levels, considered in order — and the single cheapest decision, made at design time, did more than any amount of PPE could have.
Common Mistakes and Safety Notes
- Starting at PPE. Selecting PPE before exhausting the higher controls inverts the hierarchy; PPE is the least effective level and is chosen last, never first and never alone.
- Treating the hierarchy as a menu. The methods are ranked most-to-least effective and must be considered in descending order for each risk assessment.
- Stopping after one pass. Application is iterative — evaluate the remaining risk and reapply the hierarchy until the risk is acceptable.
- Confusing de-energizing with design elimination. Placing installed equipment in an electrically safe work condition reaches elimination’s end state through other controls, with human-error potential at each step; true removal of the hazard is still the first thing to attempt.
- Leaving the top of the hierarchy to the field crew. Elimination and substitution are design and purchasing decisions; by the time equipment is installed, they may be impractical or impossible.
- Assuming one level is enough. Real tasks usually need several levels combined — barriers, awareness, instructions, training, and PPE together — before the remaining risk is tolerable.
Summary
Informative Annex F.3 ranks six risk control methods from most to least effective: elimination, substitution, engineering controls, awareness, administrative controls, and PPE. Table F.3 anchors each with an example — an electrically safe work condition, a 120 V control circuit traded for 24 V, guarded energized parts, warning signs, procedures and job planning tools, and shock and arc flash PPE. The hierarchy is applied in descending order and then reapplied, iteratively, evaluating the remaining risk after each pass until it is acceptable. The top of the ladder is cheapest at the design and equipment-selection stage, where elimination and substitution are still paper decisions with lifetime effect; the bottom of the ladder, PPE, protects only against the consequences of an event it does nothing to prevent — which is why it is selected last, after every other control has been exhausted.
Quick-Check Questions
- List the six levels of the hierarchy of risk control in order, most effective first.
Answer: Elimination, substitution, engineering controls, awareness, administrative controls, and PPE. - What substitution example does Table F.3 give?
Answer: Replacing 120 V control circuitry with 24 Vac or Vdc control circuitry to reduce the energy a worker can be exposed to. - Why is PPE ranked last?
Answer: It is the least effective control — it does not remove the hazard or prevent the event, it only reduces injury when the event happens, so it is selected only after all other controls have been exhausted. - What does “iterative” application of the hierarchy mean?
Answer: After controls are applied, the remaining risk is evaluated and the hierarchy is applied again, repeating until the risk of injury is reduced to an acceptable level. - Why are elimination and substitution best addressed at the design stage?
Answer: At design and equipment selection they are low-cost decisions on paper; once equipment is installed, eliminating or substituting the hazard may be impractical, while the design decision affects safety for the equipment’s whole life.
Based on NFPA 70E (2024), Informative Annex F, paraphrased for study.
Video lesson for this module is in production — coming soon.
Quiz for this module is being prepared.
Flashcards for this module are being prepared.
